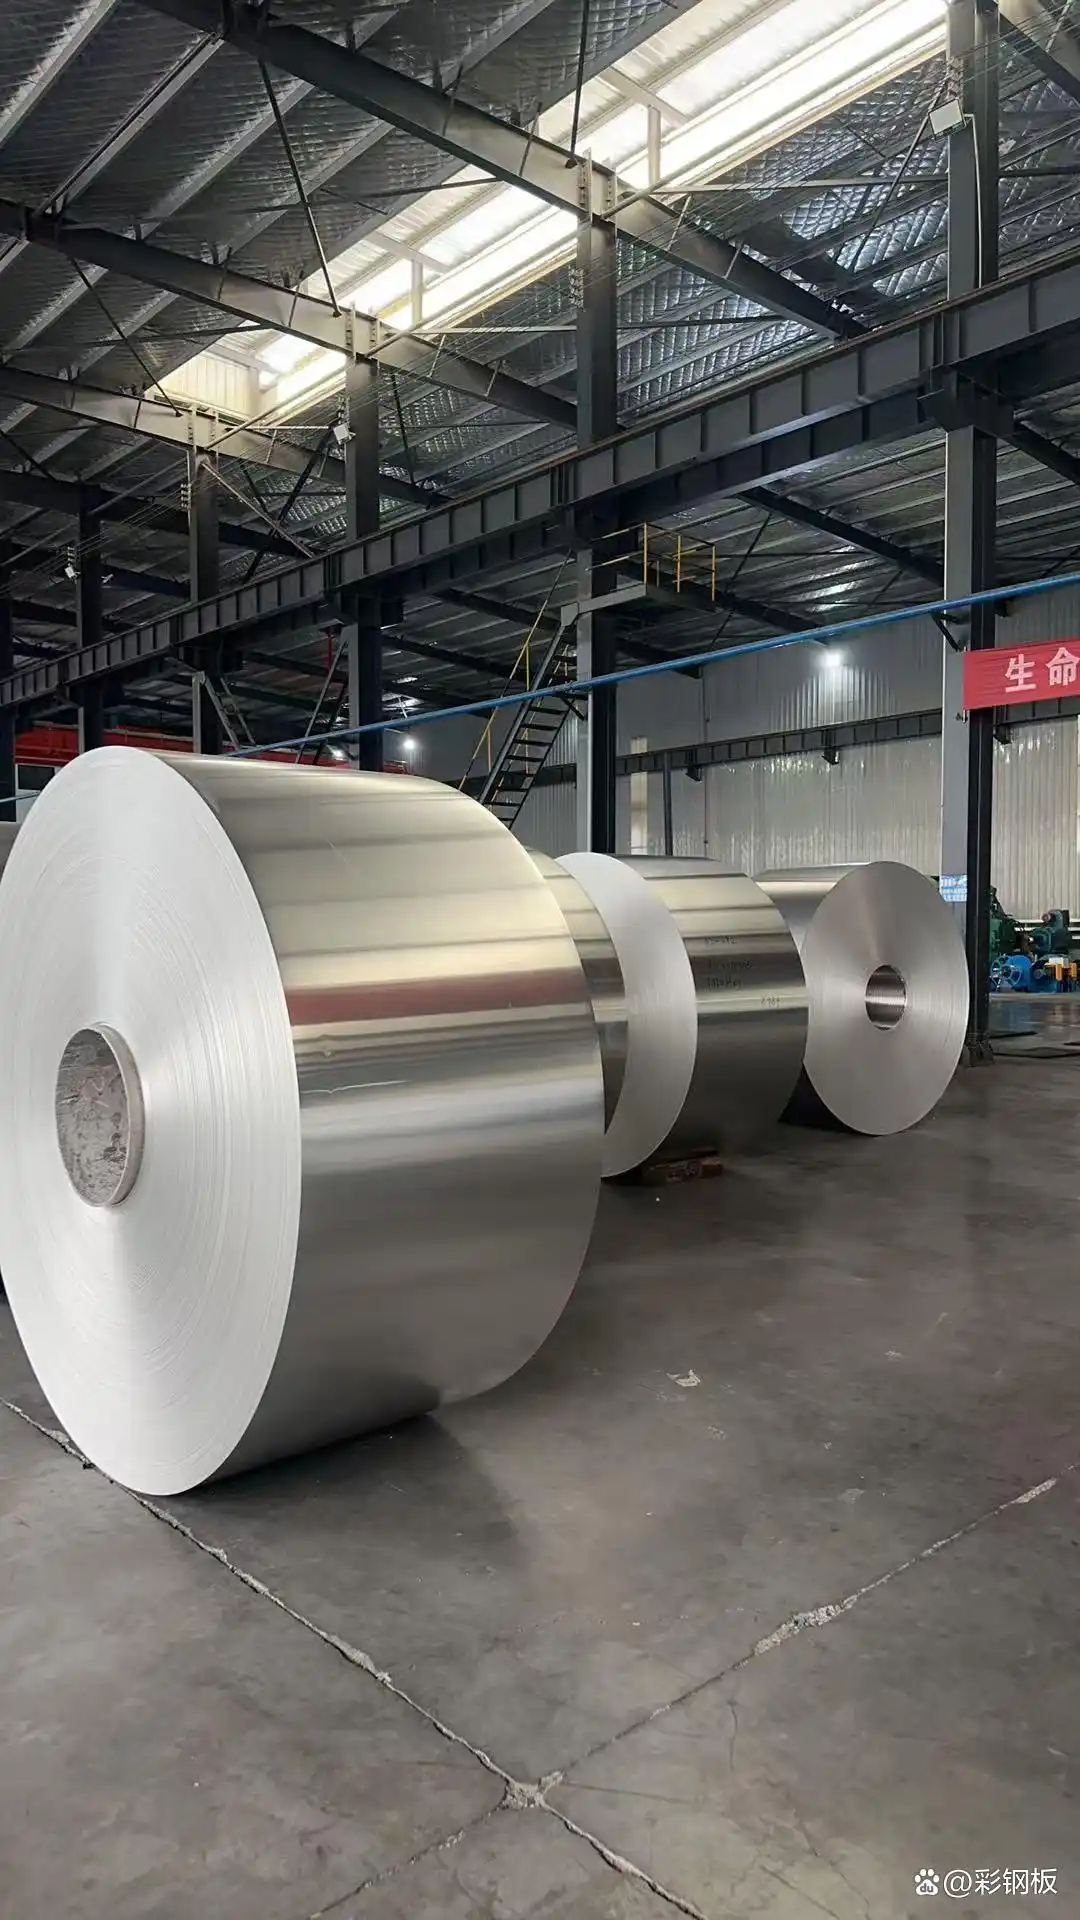
Explore our premium product portfolio engineered for superior industrial performance, high precision, and strict international compliance standards.
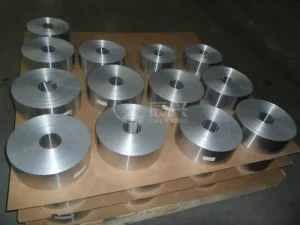
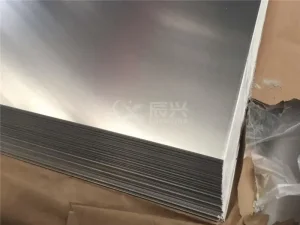
Unmatched industry experience, strict quality control systems, and global reliability making us the premier partner for industrial buyers.
Decades of metallurgy and cap manufacturing excellence.
Trusted by multinational supply chains worldwide.

Intelligent tracking ensures zero-defect delivery.

Instant support and professional 8D problem resolution.
As a leading China Aluminum Cap Manufacturer & Factories ecosystem, our operations bridge the gap between heavy metallurgy and precision consumer/industrial packaging. The global transition toward sustainable, recyclable, and tamper-evident sealing solutions has propelled aluminum caps into the forefront of modern packaging engineering.
In contemporary industrial manufacturing, aluminum caps serve critical containment functions across pharmaceutical vials, beverage bottles, cosmetic containers, and chemical receptacles. Unlike plastic alternatives, aluminum offers infinite recyclability without degradation of mechanical integrity, aligning perfectly with global ESG (Environmental, Social, and Governance) mandates and circular economy initiatives.
China's industrial clusters provide an integrated supply chain advantage—from electrolytic primary aluminum smelting to precision deep-drawing and automated anodizing. This seamless ecosystem empowers global brands to secure high-volume production schedules with reduced lead times and optimized cost structures.
Utilizing high-purity alloy series such as 1050, 1060, 3003, and specialized food-grade coatings, our factories ensure superior formability, corrosion resistance, and barrier protection against moisture, UV rays, and microbial contamination.
Navigating international regulatory frameworks requires rigorous adherence to localized standards including FDA, ISO 9001, REACH, and RoHS directives. Our engineering teams work in tandem with overseas clients to ensure full compliance across diverse regulatory jurisdictions.
Routinely deployed in antibiotic vials, infusion bottles, and dropper assemblies where sterile barrier performance and tamper-evident tear-off mechanisms are non-negotiable.
High-end ROPP (Roll-On Pilfer-Proof) caps combining aesthetic luxury with robust mechanical torque retention, customized via offset printing and embossing.
Specialized screw caps and atomizer enclosures resistant to volatile organic compounds, aggressive solvents, and high humidity storage environments.
Our foundational aluminum manufacturing expertise extends far beyond caps, empowering critical global industries.
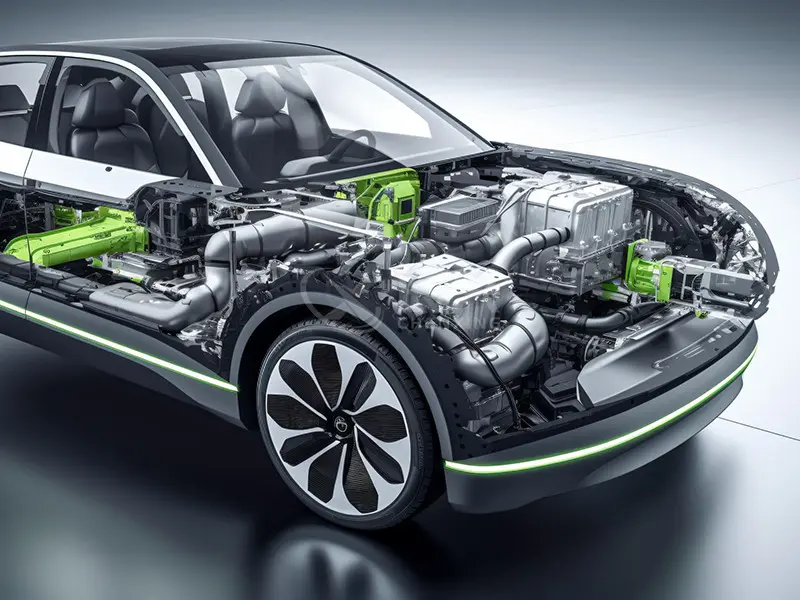
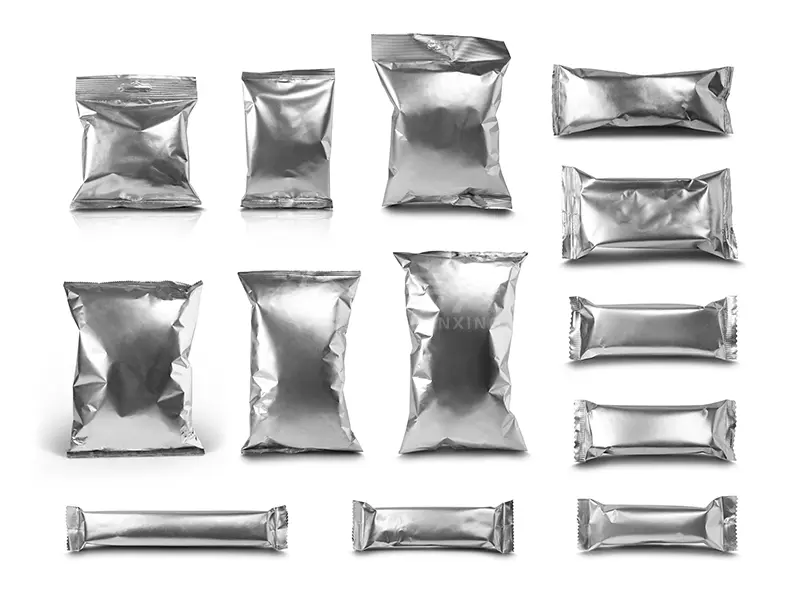
As industry pioneers, our research and development divisions are actively investing in smart packaging integrations and ultra-thin gauge metallurgy. The next decade will witness the integration of IoT-enabled traceable micro-chips within aluminum cap structures, alongside nanotechnology-based anti-counterfeiting coatings.
Development of conductive alloy traces embedded in bottle caps that instantly signal structural compromise via near-field communication (NFC).
Optimizing cold-rolling tolerances to reduce cap weight by 15% without sacrificing tensile strength, lowering carbon footprints for global brand owners.
Transitioning entirely to water-based, solvent-free organic coatings that eliminate VOC emissions during production processes.
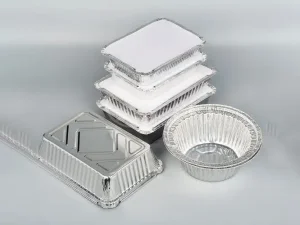
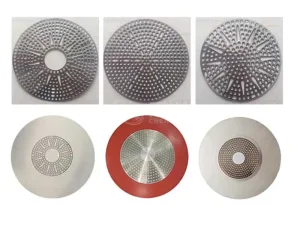
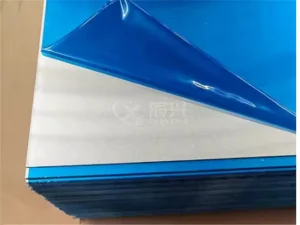
Discover our comprehensive inventory of aluminum sheets, circles, and specialized foils designed for extreme industrial environments.
Expert insights addressing key buyer inquiries regarding aluminum cap manufacturing, quality standards, and logistics.
For inquiries about our products or pricelist, please leave your message below and our engineering team will be in touch within 24 hours.
Stay updated with global aluminum market trends, technological breakthroughs, and company updates.